Table of Contents
Finger Joint Core Plywood: Checking Voids Before Machining
Finger joint core plywood should be evaluated against a defined production task. For hardware-bearing plywood components, the priority is to inspect the locations where connectors and routed edges meet the core. That turns a broad material search into a decision about the finished component, the process needed to make it and the evidence required before a repeat order.
This guide focuses on that specific buying situation. The useful next step is to cut trial pieces from several sheet positions. In particular, avoid accepting an attractive face without checking internal discontinuities. A clear sample and written specification make it easier to compare finger joint core plywood offers without relying on a surface photograph or an undefined quality claim.

The decision for hardware-bearing plywood components
Begin the finger joint core plywood evaluation by separating the part requirement from the general product description. The finger joint core plywood buyer needs to inspect the locations where connectors and routed edges meet the core; the workshop needs a repeatable way to produce the approved result. Put those two responsibilities on one trial sheet with the component drawing, material identity and acceptance decision.
For hardware-bearing plywood components, use the final viewing position and the hardest production detail to define acceptance. Record what the supplied finger joint core plywood sample represents and what it leaves unresolved. If a finish, hardware arrangement or service condition changes, revisit the relevant trial before assuming the original result still applies. The goal is a finger joint core plywood order the receiving team can inspect and the workshop can reproduce.
Define acceptance before inspecting the shipment
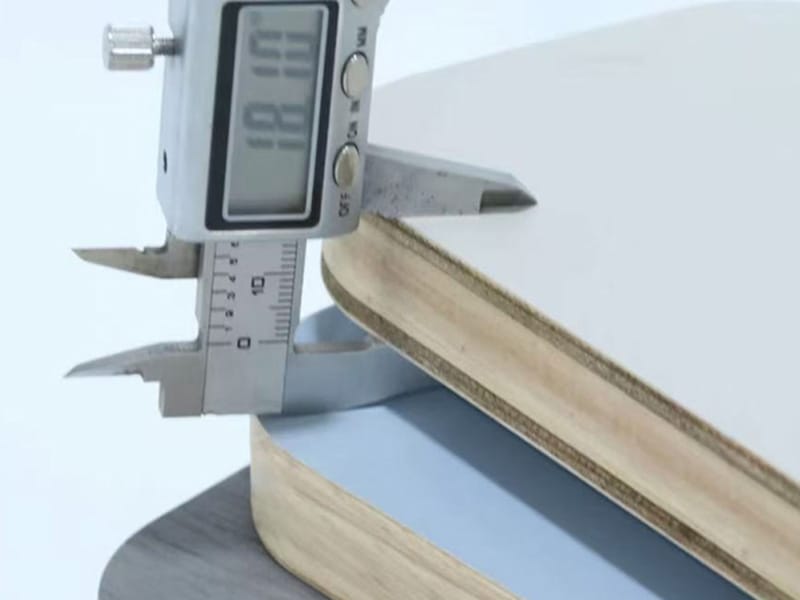
An inspection works best when the buyer and supplier share a clear acceptance basis. For finger joint core plywood, identify dimensional limits, visible-face requirements and the specific production operation that must succeed. Use measurements where practical and a reference sample where appearance needs judgment. Undefined requests for perfect quality are difficult to apply consistently.
Choose representative samples from the commercial lot and record where they came from. Inspect both the most visible surface and the detail most likely to fail in production. The receiving record for finger joint core plywood should include the lot, sample position, observation and resulting action. This makes a rejection traceable and prevents an isolated attractive sample from standing in for a shipment whose other packs have not been assessed.
Record what finger-jointed construction means
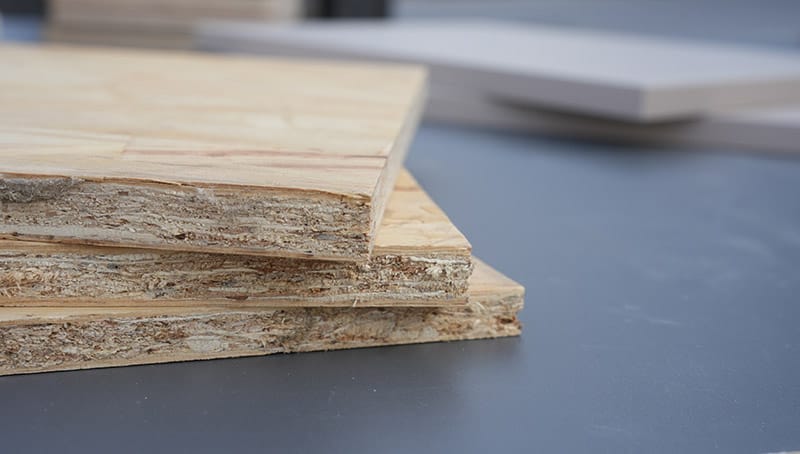
Finger-joint terminology can refer to different elements within a product description. A solid-wood panel made from jointed strips is different from plywood containing jointed core material. For finger joint core plywood, ask the supplier to locate the jointed material on a construction drawing. Inspect the corresponding cut section rather than inferring the full construction from the trade name.
Match the sample to the operation that matters, such as edge exposure, hardware installation or final finishing. If a quote includes a film face or a claimed service performance, evaluate that evidence separately. Approval of finger joint core plywood should identify the actual panel layers, joints and intended use. Clear terminology helps purchasing teams compare equivalent constructions and gives the workshop a realistic basis for its machining trial.

Inspect the finished surface from the normal viewing position
Surface approval should reflect how the product will be seen and used. For finger joint core plywood, review the final face, edge and adjacent components under realistic light. Distinguish raw-material texture from handling damage and from a finishing defect so each observation leads to the correct action.
Agree on the visible faces and retain a reference that shows the accepted appearance. Inspect dark or high-gloss surfaces particularly carefully for cut-edge damage and handling marks. With finger joint core plywood, judge the completed component rather than one attractive swatch. This gives the receiving team a practical visual standard and helps the workshop avoid unnecessary rework on concealed areas while maintaining consistency at prominent joints, corners and long runs of neighboring panels.
Look for core discontinuities at critical details
Internal gaps and overlapping material can become visible during routing or drilling. Their importance depends on where they fall in the final component. With finger joint core plywood, cut trial pieces through areas that will carry hardware, show an exposed edge or receive a deep profile. Inspect more than one small sample from a single sheet corner.
Document acceptable and unacceptable conditions with the supplier before batch production. A hidden discontinuity beside a fixing may matter more than an isolated appearance variation on a covered face. Qualifying finger joint core plywood around the critical details helps prevent a good-looking delivery from failing later in machining. Keep rejected examples and lot identifiers so the supplier can investigate the construction rather than relying on a vague complaint about quality.
Connect process records to a practical trial
A manufacturing description explains how a material is made, but purchasing approval depends on the supplied product. For finger joint core plywood, ask which process stages control the property relevant to the application and how the commercial lot is identified. Request records that can be matched to the trial material rather than a generic presentation of factory capability.
Use a production sample to check the resulting operation: cutting, routing, bonding, assembly or finishing. Compare the trial findings with the stated specification and document any exceptions. An audit of finger joint core plywood is more useful when it produces a clear control sample and change-notification requirement. The buyer then has a basis for evaluating repeat batches instead of relying on an impressive equipment list to establish product consistency.
Preserve veneer sequence in the cutting plan
Visible grain can be broken by a cutting plan that treats every offcut as interchangeable. For finger joint core plywood, coordinate sheet orientation and component sequence before machining. Assign stable part labels to doors, drawer fronts or wall panels that need to be viewed together. Distinguish the decorative layout from purely geometric nesting.
Dry-assemble the visible set before finishing and compare it with the approved design. Confirm how spare components will be identified and stored. A high-yield cutting plan for finger joint core plywood remains useful only if the resulting parts meet the appearance requirement. Where grain continuity matters, reserve the necessary material explicitly and include that allowance in the quotation instead of expecting the workshop to recover it from random remaining pieces.
Write an RFQ that suppliers can answer consistently
A useful request for quotation describes the intended application, construction, actual dimensions, quantity and delivered condition. For finger joint core plywood, add the visible faces, exposed edges and required technical evidence. Include drawings where a text description could be interpreted in more than one way, especially for orientation, machining or finished-part dimensions.
Ask each supplier to identify deviations explicitly rather than assume that silence means full agreement. Keep the final written interpretation with the approved sample. When comparing finger joint core plywood, normalize the quotation basis, packing and delivery scope before ranking offers. This turns the RFQ into a production document that the workshop and receiving team can also use, reducing the chance that purchasing and manufacturing approve different versions of the same item.
Finish the edge as deliberately as the face
Plywood edges can be exposed, covered with veneer or tape, or incorporated into a separate trim detail. Each choice affects appearance, labor and component dimensions. For finger joint core plywood, select the edge treatment before finalizing the part size. A decorative face sample does not show the finished return at a corner or an opening.
Approve a representative edged corner, including the final finish where relevant. Check adhesion, trimming and the transition between adjacent faces under normal viewing conditions. The approval for finger joint core plywood should state which edges are visible and which are concealed. This lets the fabricator allocate the appropriate work and avoids paying for unnecessary treatment on hidden edges while leaving a prominent junction undefined.
Worked example for hardware-bearing plywood components
A receiving record can separate three observations: a measured dimension outside the signed limit, a surface feature permitted by the appearance sample, and a damaged corner caused during handling. Those observations need different actions. For finger joint core plywood, record the affected face, position and lot rather than grouping every finding under poor quality. Keep a reference photograph or measurement with each decision. Apply the same finger joint core plywood criteria across the sampled packs, and hold unresolved findings for supplier review instead of changing the acceptance basis after seeing which parts are convenient to use.
Comparison of three purchasing approaches
| Approach | What it resolves | What remains to check |
|---|---|---|
| Buy from a face sample | Initial color or texture preference | Core, finished detail, component fit and documented use |
| Buy to a written construction | Defined material, dimensions and delivered condition | Whether the workshop can produce the intended finished part |
| Approve a representative finished trial | Construction and processing tested on the relevant component | Commercial-lot consistency and any later material or process changes |
For finger joint core plywood in hardware-bearing plywood components, the third approach usually provides the clearest evidence for this decision: inspect the locations where connectors and routed edges meet the core. It also makes the limits explicit. A finished trial covers its documented construction and conditions; it does not qualify every product sold under the same material name.
A practical trial for this order
Identify the requirement: inspect the locations where connectors and routed edges meet the core. Add the drawing revision, intended environment and delivered material construction to the trial record.
Prepare representative finger joint core plywood samples from the proposed commercial construction. Include both the visible face and the critical machined or assembled detail.
Run the agreed verification: cut trial pieces from several sheet positions. Use the intended equipment, adjacent components and finishing route so the result represents normal production.
Record acceptance and unresolved questions. Specifically check whether the process risks accepting an attractive face without checking internal discontinuities. Keep extra repair or finishing labor visible in the cost comparison.
Retain the approved finger joint core plywood sample and transfer the same specification to the purchase order. Review a substitution or changed process before releasing the affected repeat batch.
For background on wood structure, moisture, composite panels, joints and finishing, consult the USDA Forest Products Laboratory Wood Handbook. This independent technical reference supports material understanding; it is not a certification or test report for any DA AO product.
Discuss the specified construction with DA AO
DA AO lists melamine-faced plywood within its panel range. Its wood-panel services describe customization of size, thickness, surface finish and decorative pattern. Send the proposed application and drawing so the available construction can be checked against the requirement before quotation.
For a finger joint core plywood inquiry about hardware-bearing plywood components, include dimensions, quantity, required finish, exposed edges, hardware or fixing details and the evidence needed for approval. Ask the team to confirm the supplied construction and sample arrangement in writing. Use the inquiry form after the FAQ to request a specification review and a quotation based on the same information.
Frequently asked questions
What is the first check when buying finger joint core plywood for this application?
For hardware-bearing plywood components, first inspect the locations where connectors and routed edges meet the core. Identify the supplied construction and put that requirement in the quotation request so the supplier and workshop evaluate the same finished component.
What sample should I request for finger joint core plywood?
Request representative commercial material, then cut trial pieces from several sheet positions. Keep the drawing, material identity and process conditions with the result. A sample that omits the critical detail cannot establish whether that detail will work in production.
Which mistake should this finger joint core plywood order avoid?
Avoid accepting an attractive face without checking internal discontinuities. Agree on the intended construction, finished detail and acceptance method before batch processing, then check a representative commercial lot against the retained approval.
Can a supplier substitute another finger joint core plywood construction?
Review the proposed change against the signed specification and the critical trial. A matching name or finish does not establish equivalent machining, fit or service behavior. Obtain written approval and repeat the affected evaluation where necessary.
What should a finger joint core plywood quotation include?
Include actual dimensions, quantity, supplied finish, packing and delivery basis, together with the requirements for hardware-bearing plywood components. Identify sample approval and any required technical evidence separately so the commercial offer can be compared consistently.